


Requirement Definition: Write the Test Specification First, Then Discuss the Proposal
1. Define the inspection types: Categorize them into four types—surface defects, dimensional measurement, character recognition, and positioning guidance—as the technical approaches vary significantly across different scenarios.
2. Quantify Core Metrics: Refine the objective of “identifying defective products” into specific, acceptance-testable criteria, such as “detect scratches ≥0.3 mm in length with a false negative rate ≤0.5%.”
3. Define Boundary Conditions: Specify the maximum production line cycle time, on-site vibration and lighting conditions, and integration requirements with PLC and MES systems.
Core Hardware Selection: Say No to Specification Inflating

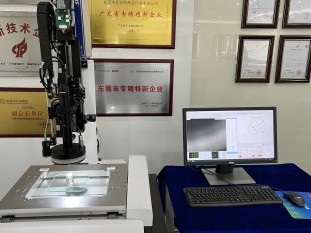
1. Industrial Cameras: Calculate the required resolution using the formula “minimum feature size = 3–5 pixels”; the frame rate must match the production line cycle time; black-and-white cameras are preferred for dimensional measurement applications.
2. Lenses: Standard fixed-focus lenses are suitable for conventional workstations, while telecentric lenses are used for high-precision dimensional measurement to eliminate perspective distortion.
3. Lighting: Over 60% of stability issues in projects are caused by improper lighting. For reflective workpieces, diffuse dome lights are preferred; for low-contrast defects, custom-wavelength light sources are required.
Vendor Selection: Prioritize the Ability to Implement Solutions in Practice

1. Prioritize in-house development: Give preference to vendors with in-house control over algorithms and core hardware, and avoid integrators that rely entirely on outsourced components and assembly to minimize buck-passing when on-site issues arise.
2. Verification through real-world case studies: Require vendors to provide production lines that closely match your specific operating conditions, rather than a generic wall of brand case studies.
3. Assess iterative capabilities: Confirm that the vendor can provide a low-threshold data annotation and training platform that enables production line engineers to independently iterate on models without relying on on-site vendor support.
Closed-Loop Cost and Acceptance: Building Certainty into the Contract
1. Understanding the Cost Structure: Hardware accounts for only 15% to 30% of the total investment; software algorithms, on-site integration and debugging, and quality assurance iterations are the core value of the solution.
2. Fixed Acceptance Criteria: Agree in advance on the statistical criteria for miss-detection and detection rates (at the pixel or image level), IOU determination thresholds, and rules for sealing blind test samples to avoid vague clauses such as “accuracy ≥ 99%.”
3. Phased Acceptance: First, conduct blind testing on sealed samples; then, perform shadow operations after deployment and compare results with manual testing; finally, conduct closed-loop operations with small batches. The final payment should be made only after all criteria have been met.
Product recommendation
TECHNICAL SOLUTION
MORE+You may also be interested in the following information
FREE CONSULTING SERVICE
Let’s help you to find the right solution for your project!
 ASK POMEAS
 PRICE INQUIRY
 REQUEST DEMO/TEST
 FREE TRIAL UNIT
 ACCURATE SELECTION
- APPICATION CASE
- RESOURCE CENTER
- DOWNLOAD CENTER
SOLUTIONS SUPPORT
- ZOOM LENS SELECTION TOOL
- TELECENTRIC LENS SELECTION TOOL
- FA LENS SELECTION TOOL
- ZOOM RATIO TABLE
- CERTIFIED MODEL
SELECTION TOOL
- WHY POMEAS
- FAQ
- PRIVACY POLICY
- TERMS OF USE
- DELIVERY & RETURN POLICY
CUSTOMER CARE
 ADDRESS
Add.:No.68, Yongwei Road, Baizhoubian, Dongcheng District, Dongguan, China,523000
CONTACT
 Tel:+ 86-0769-2266 0867
 Fax:+ 86-0769-2266 0867
 E-mail:marketing@pomeas.com
Wechat QR code
Software Copyright :2021SR0176001 抄袭必究, 技术支持:誉新源科技